Splicing Press Machine
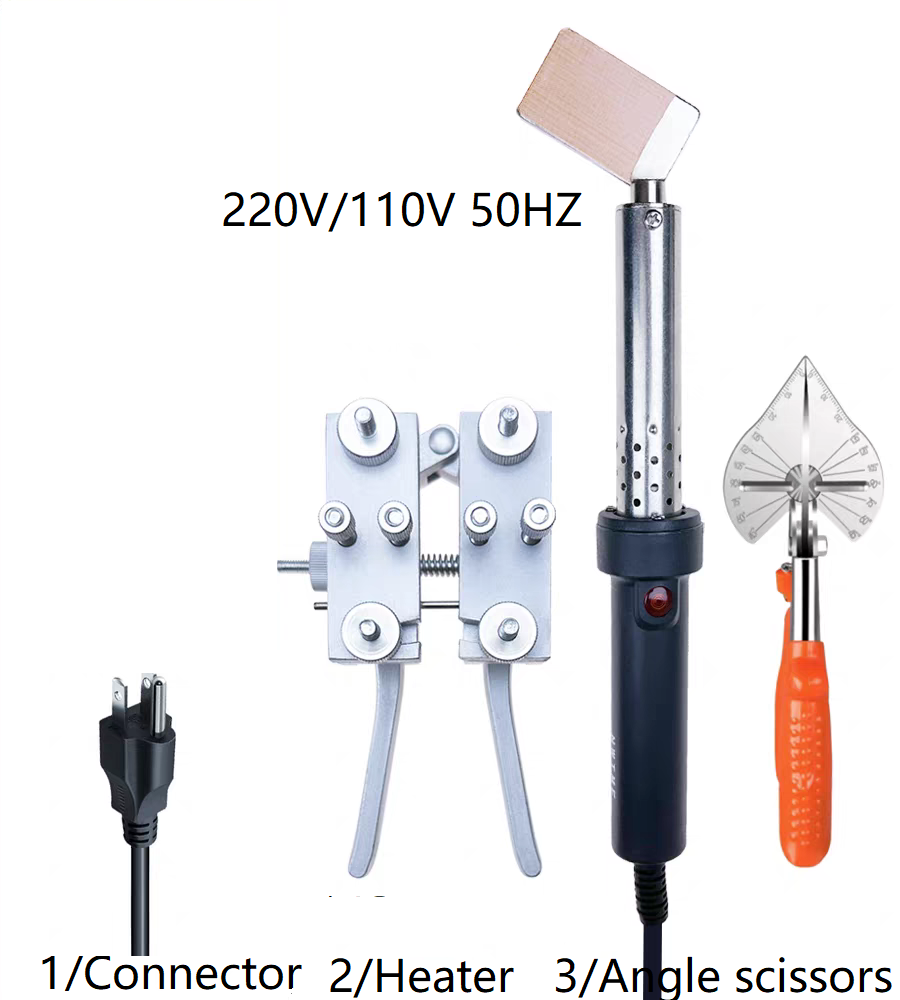
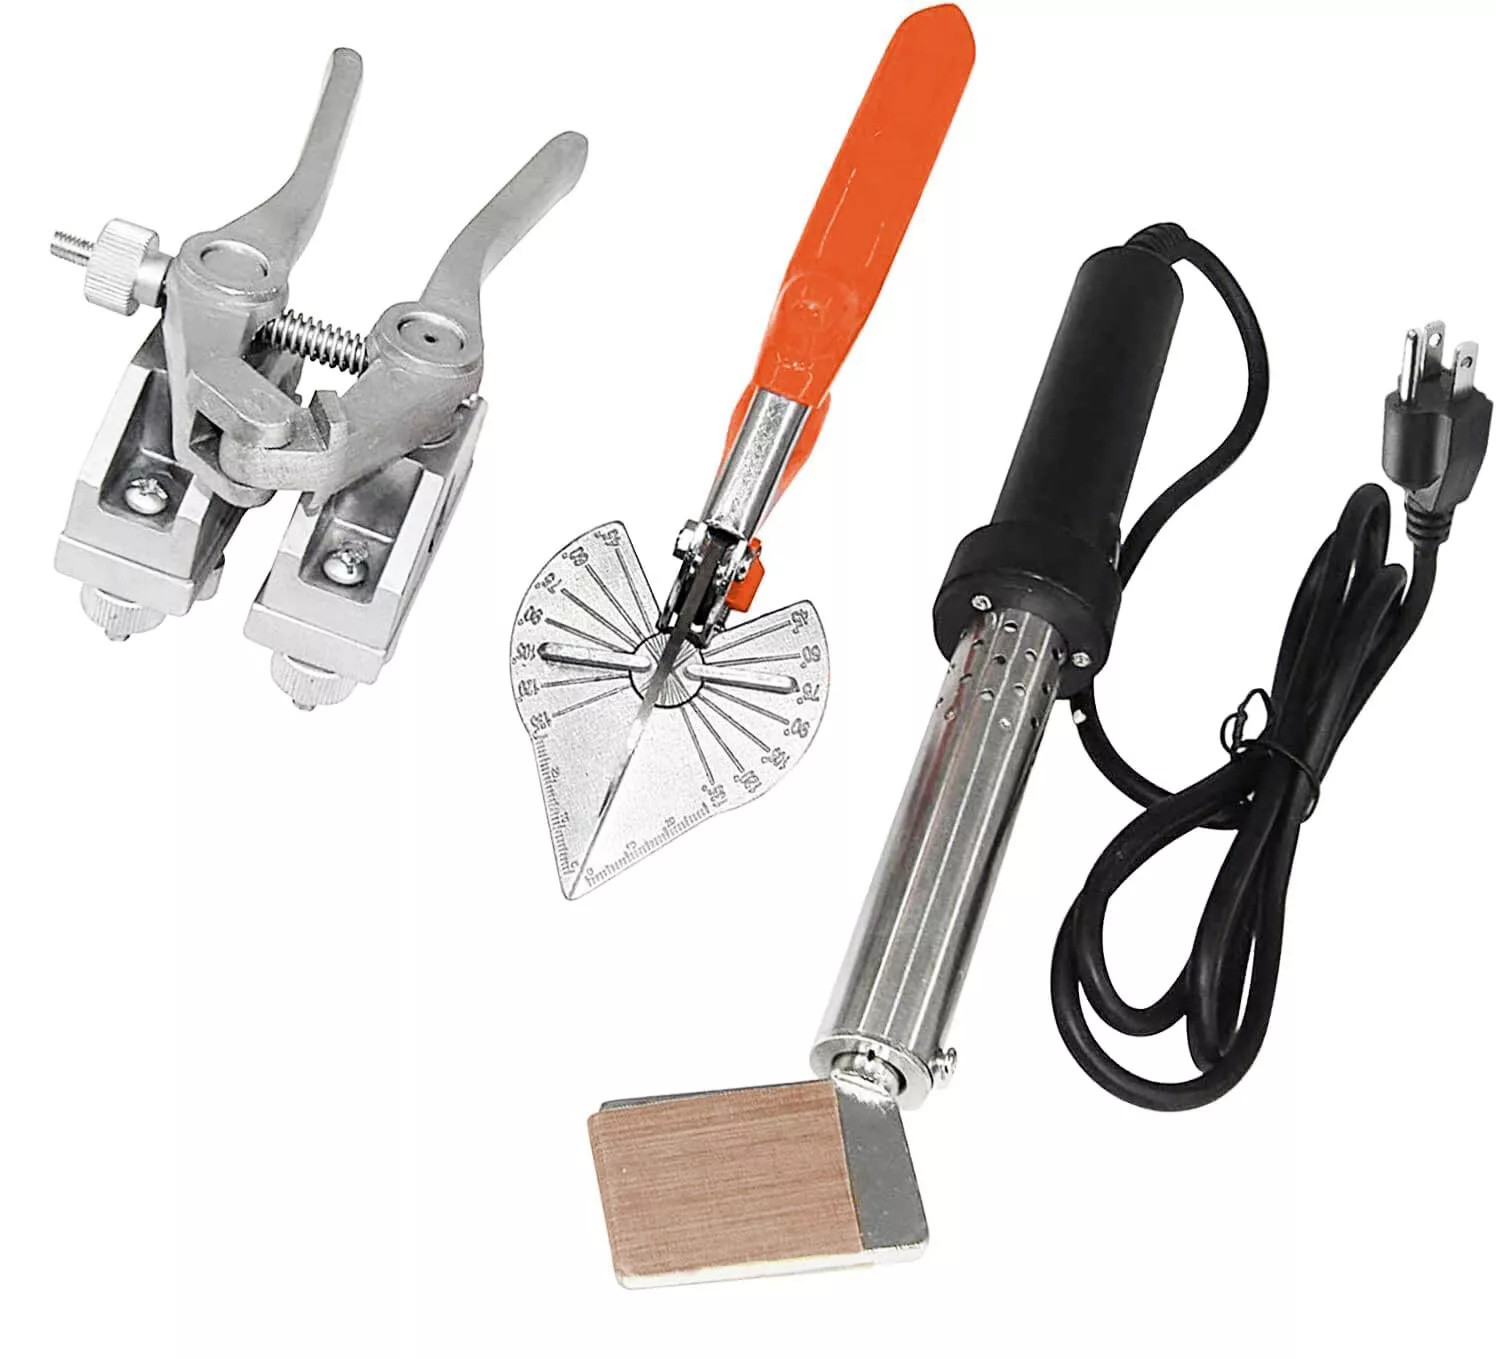
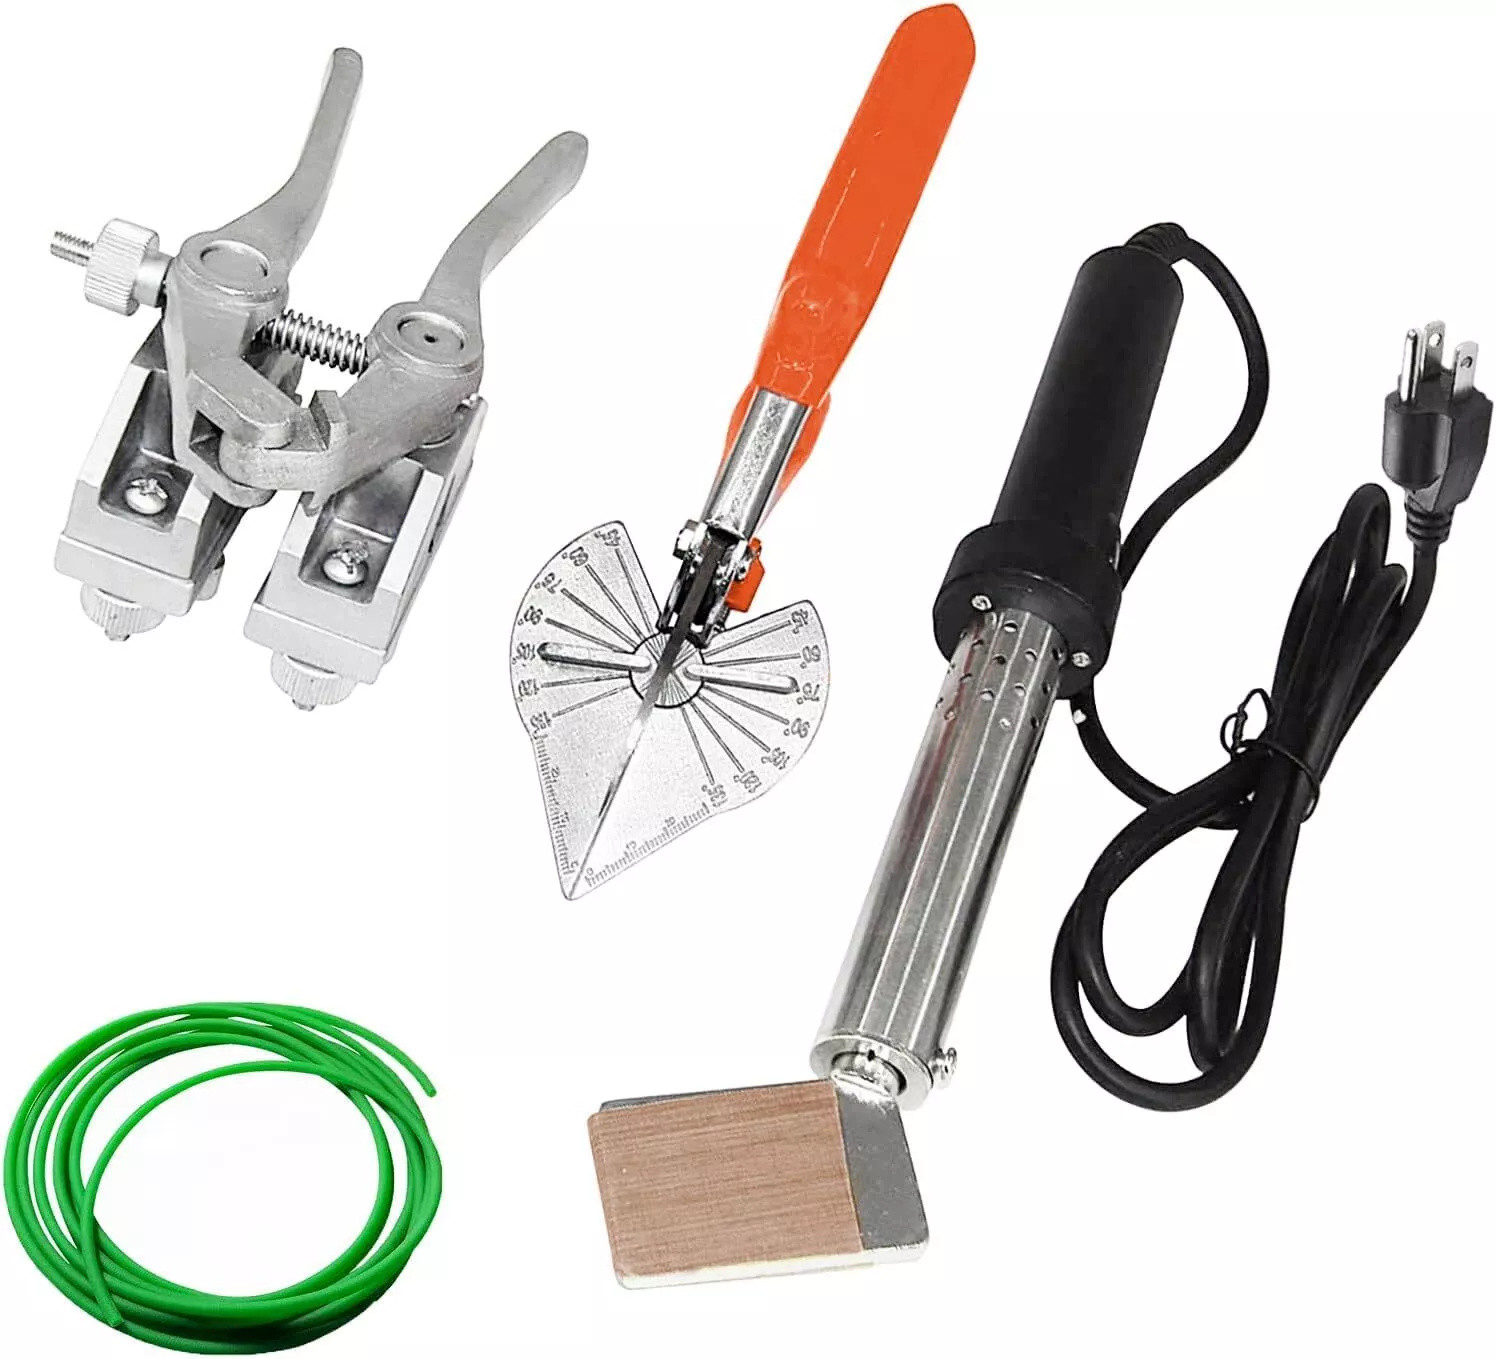
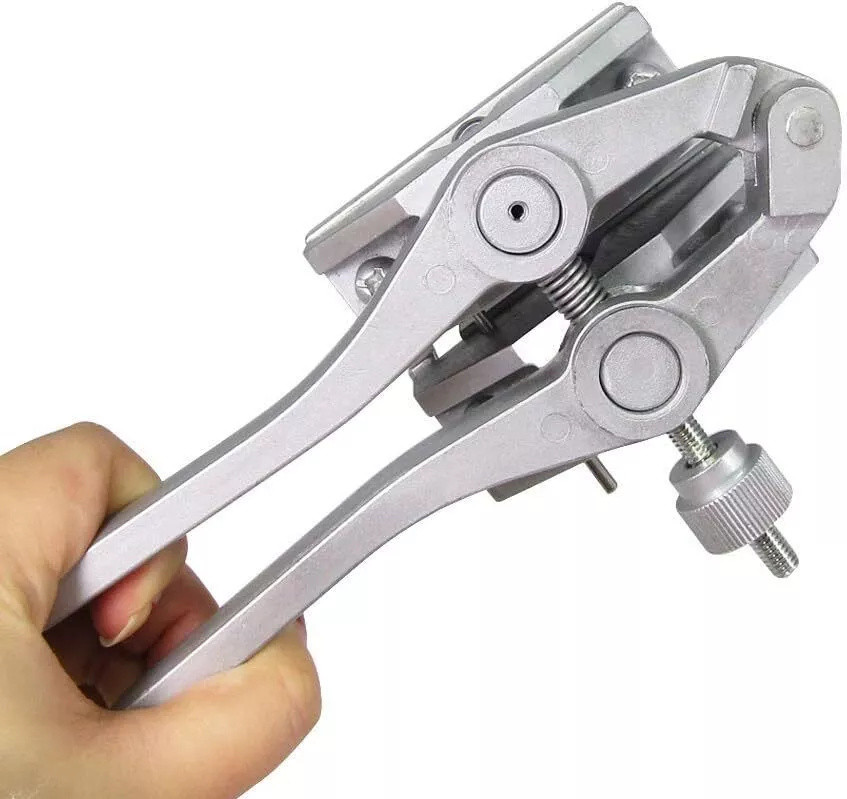
Round belt Splicing kits
PU round belt splicing/Connect kits
Conveyor & Industrial Belt Fabrication Equipment
Round Belt Splicing Kit
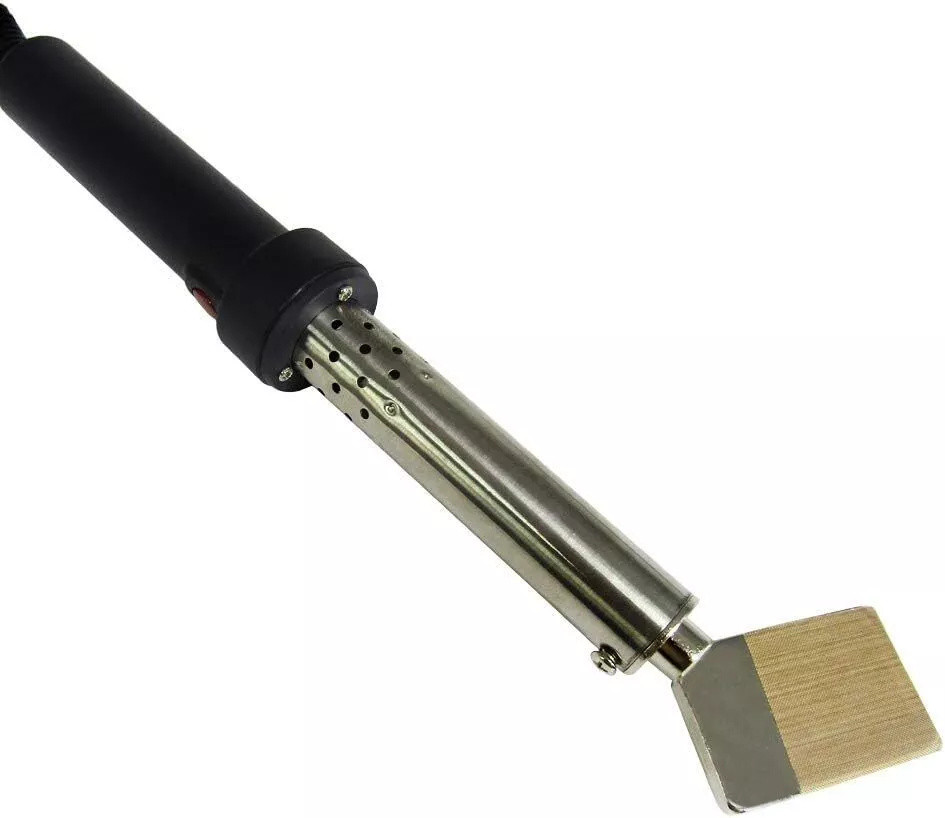
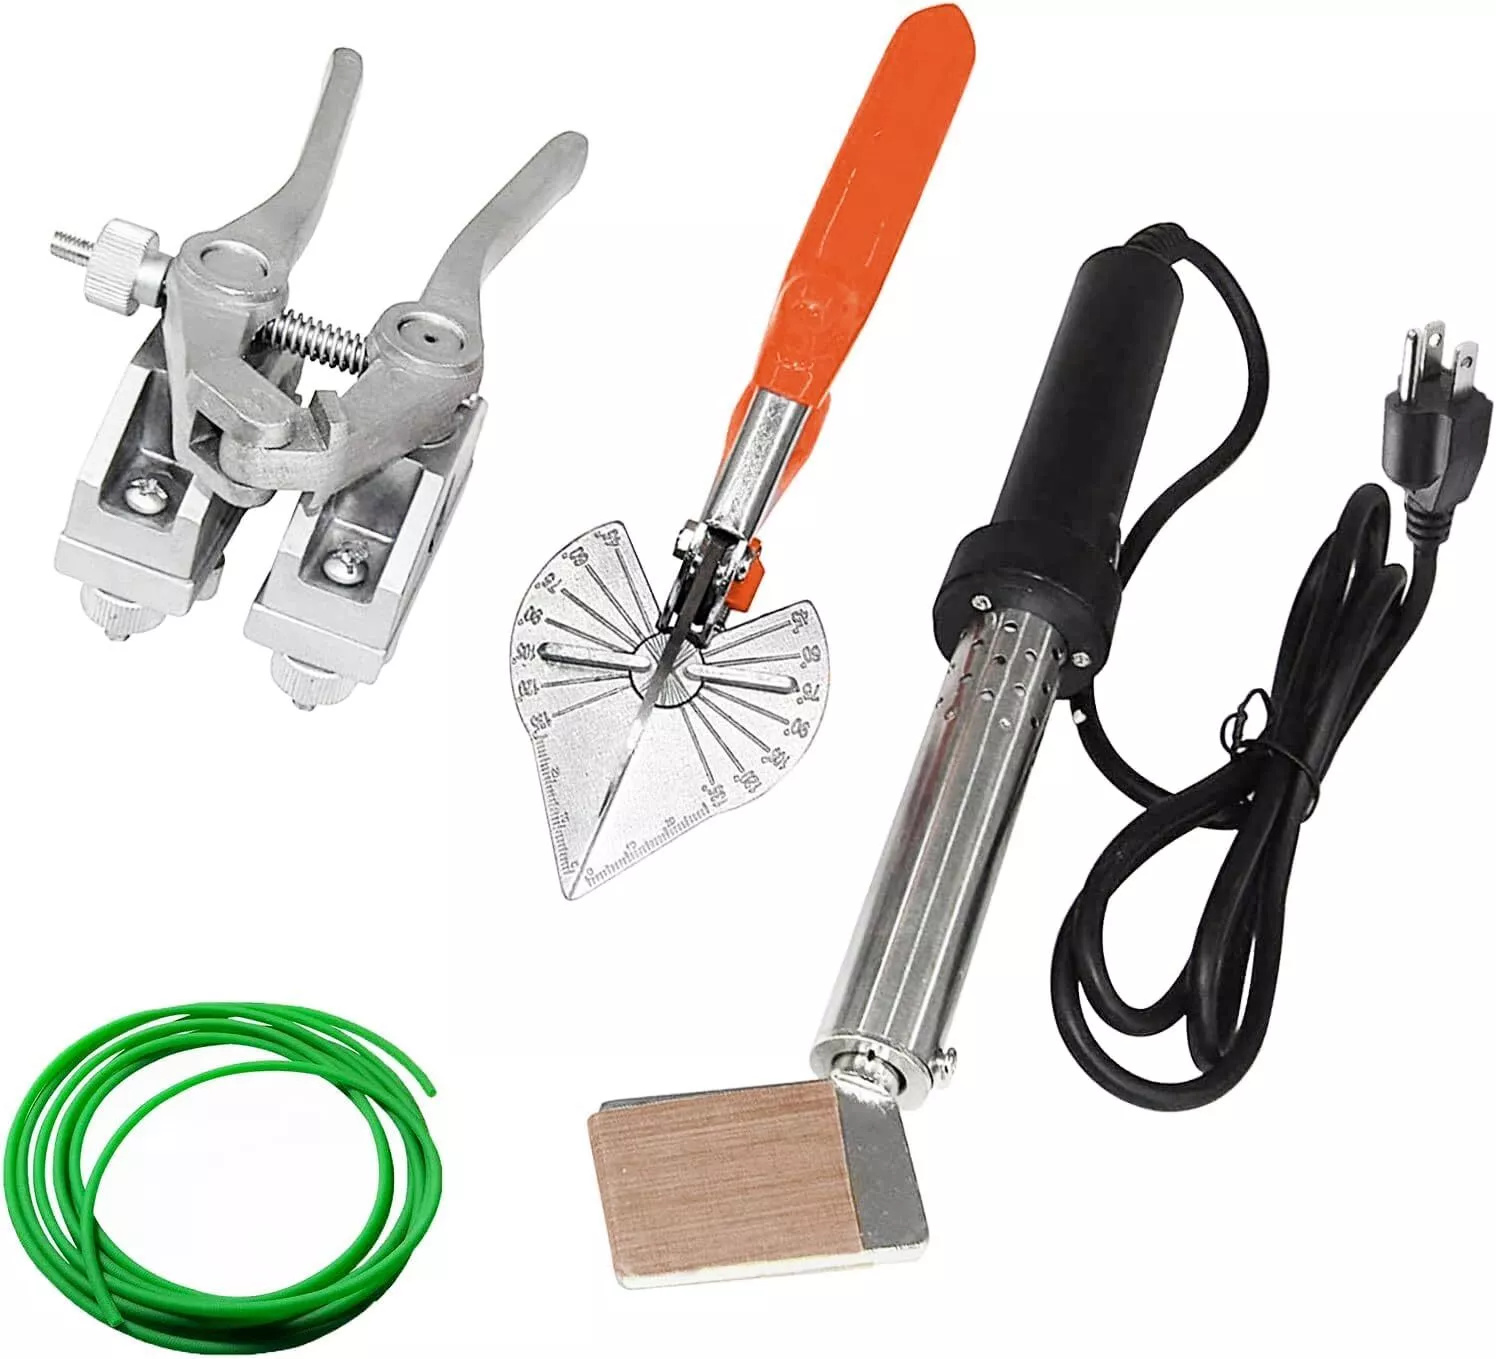
Bevel Shear + Alignment Clamp + Constant-Temperature Heater
PU round belt · V-belt · pentagonal belt · PU cord | Φ2–Φ20 mm | 3–8 min per splice
▎Product Overview
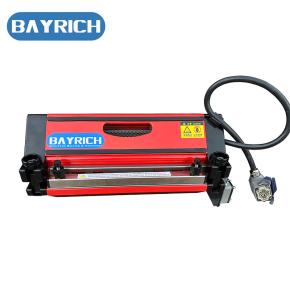
| An on-site splicing kit for PU / TPU round belts, V-belts, pentagonal belts and PU cord. Three core tools: a 45°–135° adjustable bevel shear, an aluminium alignment clamp and a 200 W constant-temperature heater. The shear cuts both ends to an identical bevel; the V-groove clamp holds them coaxial and face to face; the Teflon-coated tip melts both faces, after which the ends are butted together and left to cool into an endless belt. Everything packs into a blow-moulded case. Splicing is done on the machine without dismantling — about 3–8 minutes per joint, with joint strength up to 80% of the original belt. |
▎Technical Specifications
Item | Specification | Item | Specification |
Model | W-25 Round belt splicing kit | Heater power | 150 W |
Belt diameter | Φ2–Φ20 mm (std Φ2–13) | Temperature | 0–350 °C stepless |
Heating tip | Teflon-coated, replaceable | Working temp. | 250–300 °C typical |
Bevel shear | 45°–135°, SK5 blade | Stability | ±5 °C constant |
Clamp | Aluminium, Teflon-lined V-groove | Power supply | 220 V / 50 Hz (110 V opt.) |
Heat / hold | 30–90 s / 3–5 min | Weight | 3.5 kg with case |
▎Key Features
● Complete set—shear, clamp and heater; no dismantling | ● Fixed bevel—45°–135° shear keeps both ends matched |
● Teflon tip—non-stick, string-free, replaceable | ● Constant temperature—150–350 °C at ±5 °C |
● Self-aligning clamp—V-groove, no offset when pressed | ● Portable—3.5 kg blow-moulded case |
▎Applications
● Belt types—PU / TPU round belt (smooth or rough), PU V-belt, pentagonal belt, PU cord | ● Diameter—Φ2–Φ20 mm (Φ3–Φ12 most common) |
● Industries—carton sealers, folder-glurers, binding lines, packaging, textile, food and logistics conveyors | ● Not suitable—rubber, PVC and steel-cord belts (need vulcanizing or fasteners) |
▎Operating Procedure
① Cut: cut square, 5–10 mm allowance | ② Bevel: 45°, both ends identical, burr-free |
③ Clamp: load into V-groove, 2–3 mm gap, lock | ④ Heat: 250–300 °C, tip on the faces, 30–90 s |
⑤ Join: withdraw the tip, butt the ends within 30 s | ⑥ Cool: hold 3–5 min, then trim the flash |
Tip: join within 30 s of heating — oxidised faces cause cold joints. Never mix material, hardness or colour. Trim flash while still warm.
Specifications are for the standard configuration; the delivered unit prevails. Heating time and temperature vary with belt diameter, compound and ambient temperature — trial a sample first.
INQUIRY
LATEST NEWS
CONTACT US
Contact:
Phone: 0086-15669710783
E-mail: echowlq@163.com
Whatsapp:0086-15669710783
Add: 9th Floor, Building 1, No.28, Henghe 3rd Road, Ouhai Economic Development Zone, Wenzhou City, Zhejiang, China.