Industrial Belt
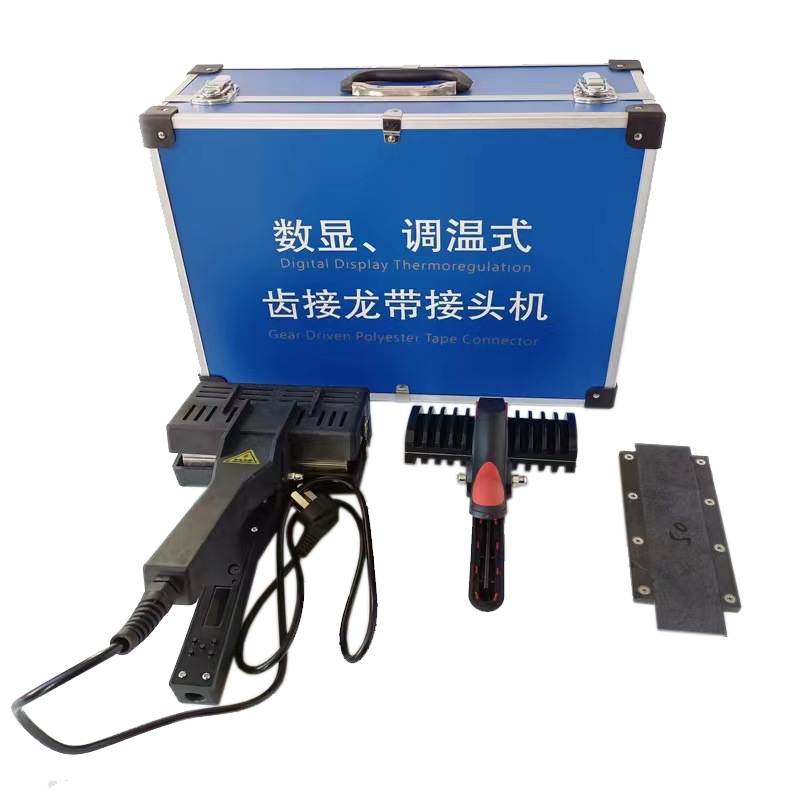
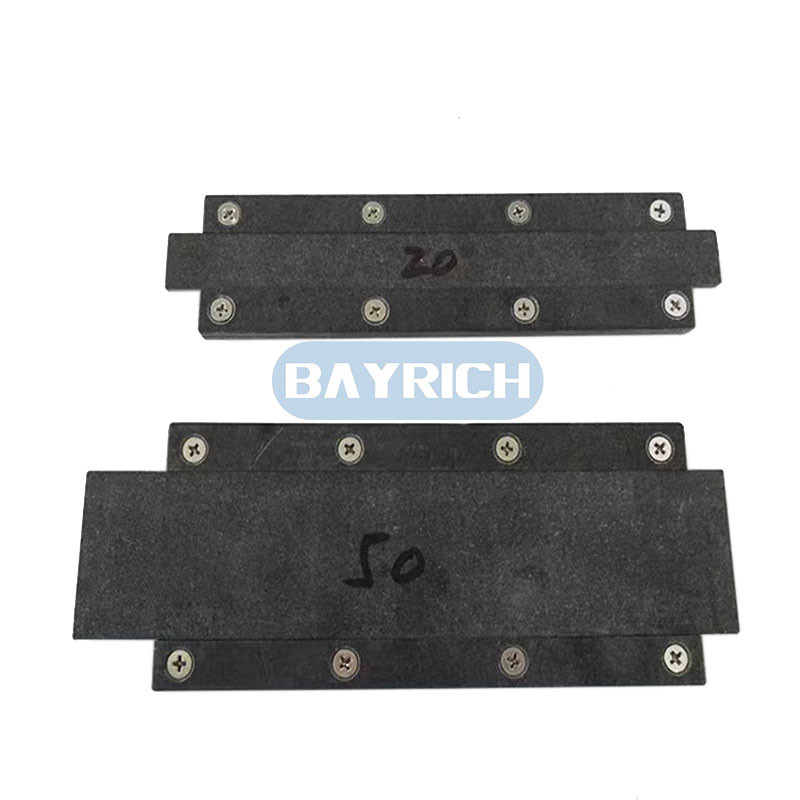
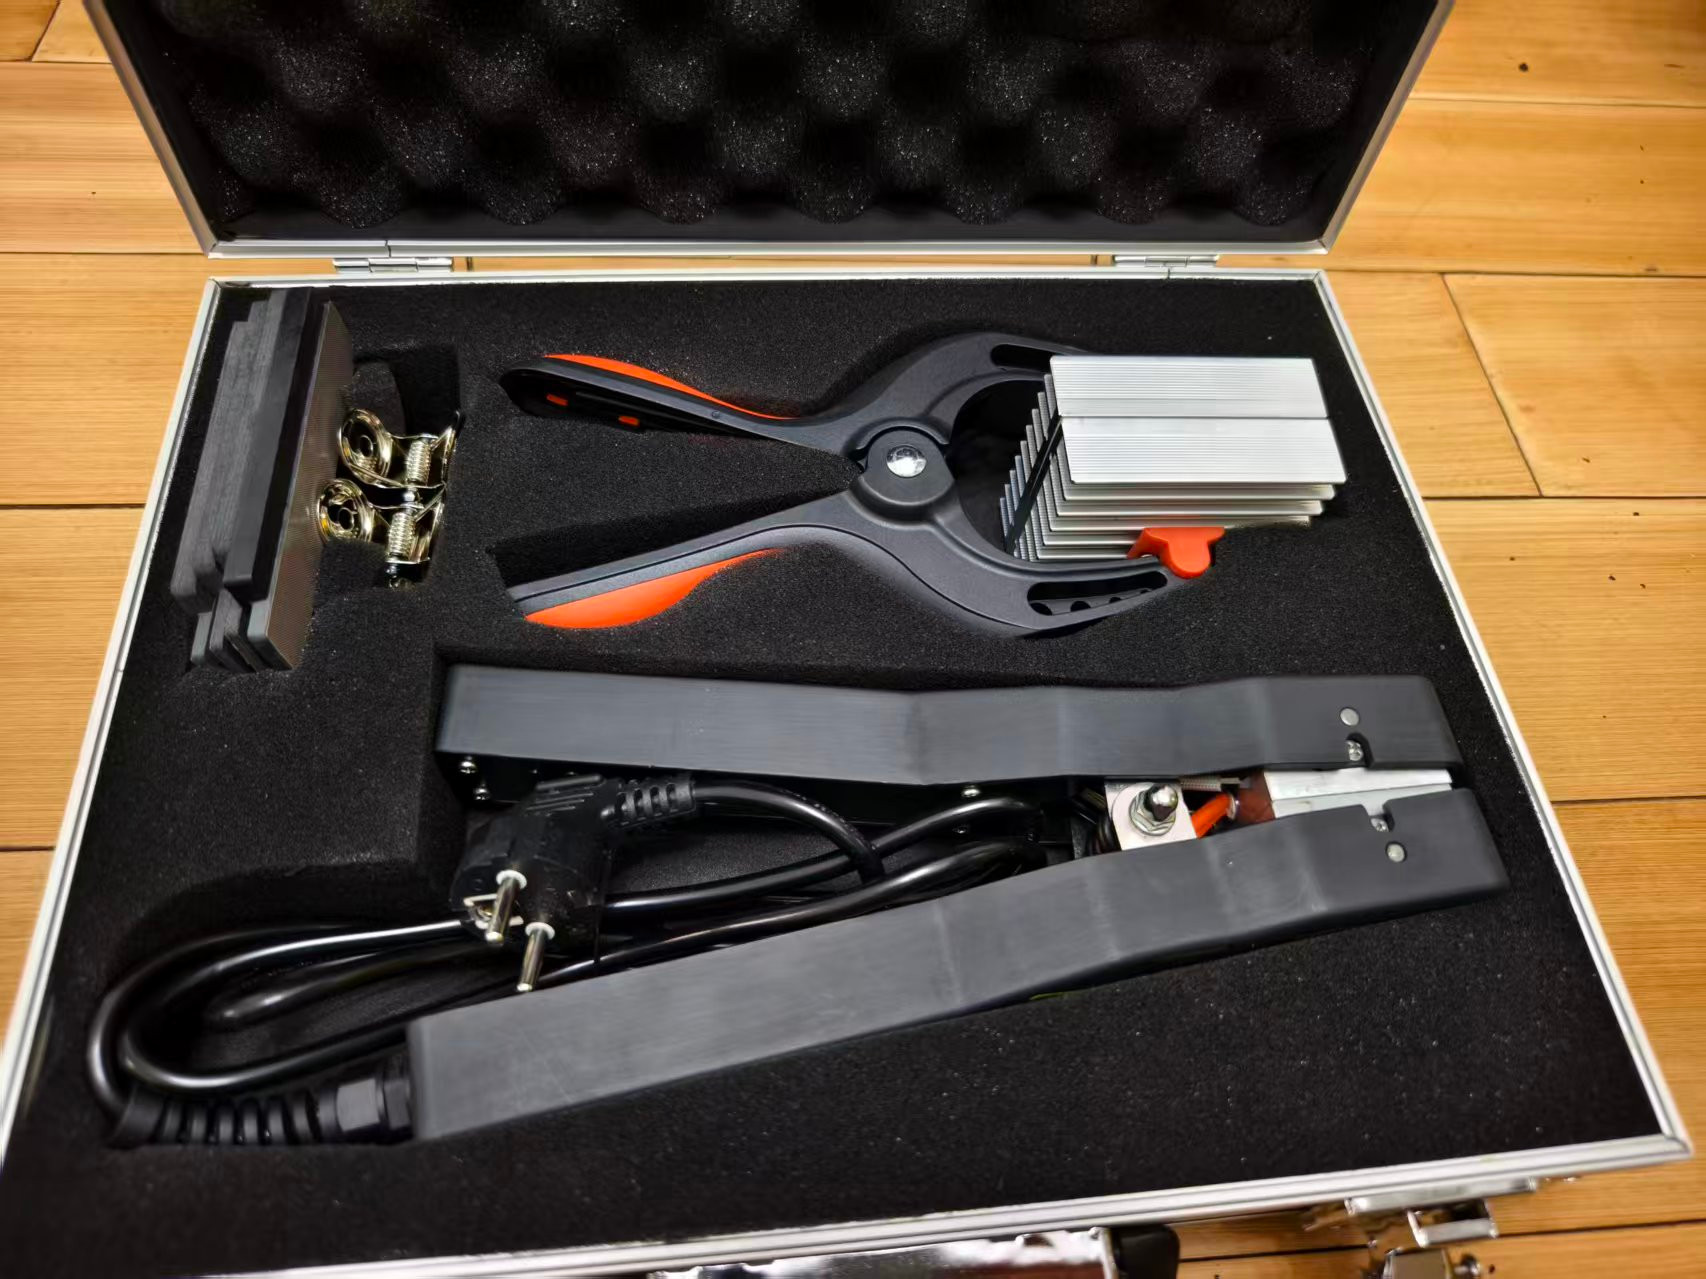
TC Belt Tangential Belt Finger Splice Kit
Digital Temperature-Controlled Tangential Belt Splicer
Conveyor & Industrial Belt Fabrication Equipment
TC Belt Finger Splice Kit
Digital Temperature-Controlled Tangential Belt Splicer
Polyester tangential (TC) belt · nylon flat belt · spindle tape | finger splice | portable aluminium case
▎Product Overview
| A portable kit for finger-spliced endless belts in TC (polyester tangential) belt, nylon flat belt and spindle tape. Both ends are punched into interlocking fingers, meshed, then fused under a digitally controlled heated head and cooled — the joint ends up level with the belt. ● Finger splice — interlocking teeth spread the load; 85–90% of the original belt strength. ● Digital control — set and read the temperature on the panel; no scorching, no under-cure. ● Level joint — same-thickness shims keep the splice flush over pulleys. Packs into an aluminium case; the splice is made at the machine, with no shaft dismantling — about 15–25 minutes per joint. |
▎Technical Specifications
Item | Specification | Item | Specification |
Model | HJ-55/HJ-816 finger splice kit | Belt types | TC / nylon flat belt, spindle tape |
Maximum Belt width | 45 mm (HJ-55) 85mm(HJ-816) | Belt thickness | 1.0–4.0 mm |
Heating | Electric head, upper / lower | Temperature | Ambient–250 °C, digital |
Working temp. | 160–180 °C | Power | 220 V / 50 Hz, 500 W |
Heating time | 3–8 min (by thickness) | Weight | approx. 6 kg with case |
Note: tooth templates are specific to each belt family — pitch and depth must match the belt being joined; custom widths on request.
▎Key Features
● Finger splice—teeth share the load, high joint strength | ● Digital control—set and read on the panel, repeatable |
● Level joint—same-thickness shims keep it flush | ● Portable—aluminium case, mains only |
● Interchangeable templates—one tool, many widths | ● No scorching—steady heat, base film stays tough |
▎Applications
● Belt types—TC belt, nylon flat belt, spindle tape | ● Industries—ring spinning, twisting, press feed belts, packaging, paper |
● Width / thickness—10–45 mm, 1.0–4.0 mm | ● Not suitable—rubber, PVC, PU conveyor belts (need vulcanizing) |
▎Operating Procedure
① Cut: cut to length with tooth allowance, ends square | ② Punch: make two ends finger by finger puncher |
③ Mesh: fingers fully home, roots aligned, width checked | ④ Clamp: into the fixture with same-thickness shims, lock |
⑤ Heat: 160–180 °C, press and hold 3–8 min | ⑥ Cool: hold 5–10 min, trim the flash |
Tip: the two ends must be a tooth / slot pair; releasing the clamp before the joint has cooled thins and weakens it; above 200 °C the base film scorches and turns brittle.
Specifications are for the standard configuration; the delivered unit prevails. Temperature and time vary with belt compound, thickness and ambient conditions — trial a sample first.
INQUIRY


Categories
LATEST NEWS
CONTACT US
Contact:
Phone: 0086-15669710783
E-mail: echowlq@163.com
Whatsapp:0086-15669710783
Add: 9th Floor, Building 1, No.28, Henghe 3rd Road, Ouhai Economic Development Zone, Wenzhou City, Zhejiang, China.